GLP-1 medicines changed the scale of peptide demand within a few years. Manufacturers have expanded capacity to keep pace, yet supply still lags in places. That mismatch traces back to one truth. Peptide manufacturing capacity takes far longer to build than demand takes to grow.
A reactor ordered today will not produce a commercial supply for years. Companies choosing a GLP-1 sourcing partner are effectively deciding what 2027 looks like. Understanding that lag is the first step toward avoiding it.
Why Does Peptide Manufacturing Capacity Take Years to Build?
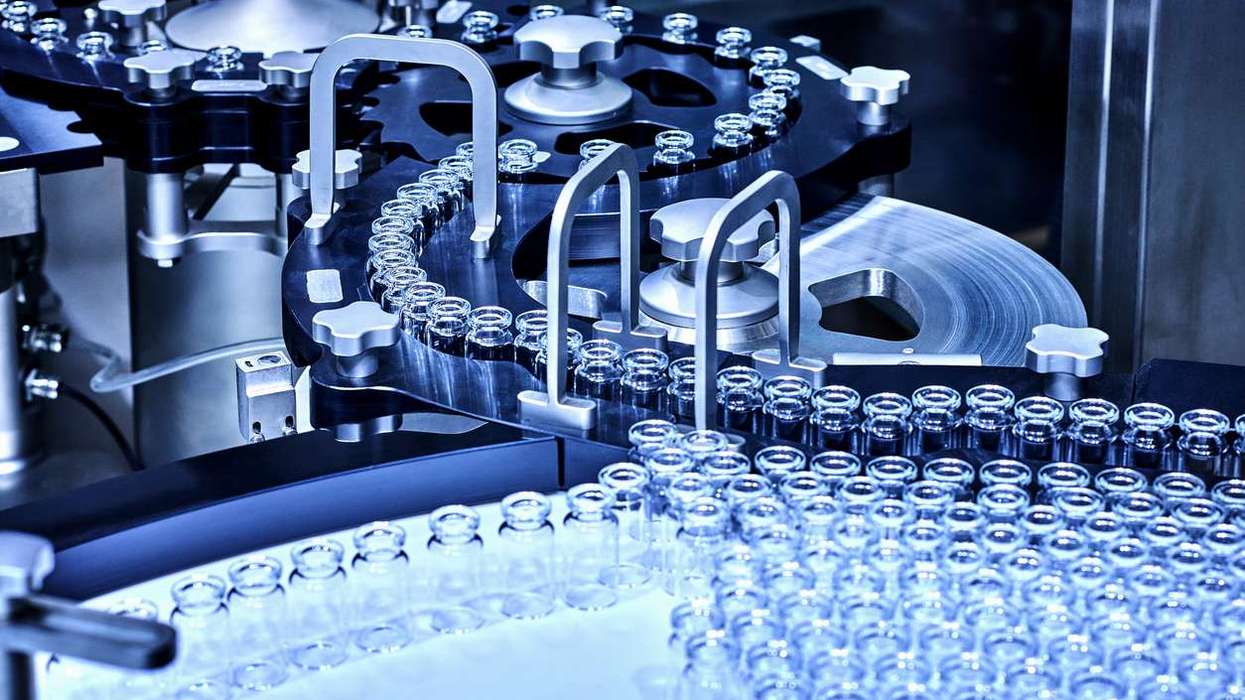
Peptide manufacturing at a commercial scale takes real time to set up correctly. A single reactor has to earn its place before running a real batch.
That process starts with ordering and installing the equipment. The equipment then has to prove it performs reliably, run after run. Only after that does it qualify to make a product for patients.
This full path routinely takes well over a year for one reactor line. Freeze-drying equipment used later in production follows a similar path. It also needs its own testing before commercial use.
Regulators add one more layer on top of this. A facility must show that its process performs consistently across several consecutive batches.
Skipping steps to save time usually backfires later. A rushed facility risks a failed inspection, which would cost far more time than careful planning would.
This is exactly why real capacity planning starts years before demand peaks. Neuland Labs builds its peptide manufacturing capacity on this longer timeline, well before a molecule reaches late-stage trials. That head start matters even more as 2027 approaches.
How Did GLP-1 Demand Outpace Existing Peptide Manufacturing Capacity?
GLP-1 demand did not rise gradually. It surged as approvals for obesity and diabetes expanded far beyond initial projections. Existing peptide manufacturing capacity simply wasn't built for a market this large. Most peptide plants before 2022 were sized for specialty drugs treating smaller patient groups. Chronic medicines prescribed to millions demand something else entirely.
Semaglutide shows this pattern clearly. The FDA listed the semaglutide shortage as active from March 2022 and declared it resolved only in February 2025. That's nearly three years between demand rising and supply catching up. Even after that, the FDA noted some regions could still see occasional shortages.
The scale of the response shows how serious the shortfall was. FDA records show the agency evaluated 48 GLP-1 API manufacturing sites to verify supply and quality. That's a large slice of the global peptide API industry, mobilized just to stabilize one drug class.
Three years reflect how long it takes to convert new demand into real peptide manufacturing output. New reactors and purification equipment take time to build and qualify, no matter how urgent the need feels.
This same pattern could repeat. Newer peptide molecules, including multi-agonist and oral therapies, are already gaining approvals. Without early capacity planning, manufacturers risk falling behind again.
What Happens When Peptide Manufacturing Decisions Are Delayed?
Delayed decisions do not cause problems right away. The cost builds quietly in the background, then surfaces all at once, usually right before launch.
Timing matters because CDMOs plan their reactor schedules years in advance. They tie committed capacity to companies that signed on early. A company that waits until late-stage trials to start looking is not choosing between many open options. It is competing with every other company that delayed the same decision, for the same limited slots.
When a company arrives late, it usually leads to:
- A launch date is pushed back, sometimes by a full commercial cycle
- A rushed technology transfer, where process knowledge moves faster than it can be properly validated
- Settling for a partner with less relevant chemistry experience, simply because they had open capacity
None of these are rare or hypothetical outcomes. They played out repeatedly during the GLP-1 shortage years, when demand outpaced available capacity. Clinicians had to switch patients to less effective alternatives. Early commitment, therefore, functions as the only lever available before demand becomes unmanageable.
Why Do Today's Peptide Manufacturing Decisions Shape the Future Supply?
It takes about two to three years for a new capacity to become fully operational. A facility expanded in 2026 still needs installation and validation before it can ship a commercial product. The FDA requires manufacturers to prove their process works reliably across multiple runs before releasing any commercial batch. This step alone can take well over a year.
That timeline cannot be shortened by urgency. A company that starts looking for a peptide manufacturing partner in 2027 is already behind. By then, most qualified capacity is already booked.
Companies securing peptide manufacturing capacity today will have a dependable supply when 2027 arrives. Those who wait will be left negotiating for whatever capacity remains.
How Can Companies De-Risk Their Peptide Manufacturing Timeline Now?
Companies can de-risk their peptide manufacturing timelines by planning years in advance. Forecasting demand three to four years out lets a company secure reactor time before rivals even start looking.
Working with more than one manufacturing partner adds a second layer of protection. Choosing a partner in a different geography reduces the risk of delays or raw material shortages at a single site. It also gives a company more room to negotiate as capacity tightens.
Getting technical teams talking early speeds things up further. Sharing process data with a manufacturing partner before a formal handover helps both sides. Scale-up problems surface early, while there is still time to fix them.
None of this guarantees a smooth supply chain. It does meaningfully raise the odds that a molecule reaches patients on schedule. Otherwise, that molecule waits behind someone else's order.
Neuland Laboratories builds its peptide manufacturing strategy around this lesson. Its facilities support solid-phase and solution-phase peptide synthesis, as well as hybrid routes, across multiple reactor scales. The FDA, EMA, and PMDA have all approved its facilities. A new peptide facility campus is adding further reactor capacity. That gives pharmaceutical and biotech companies room to plan years ahead of demand.
For companies mapping their 2027 peptide supply, the planning conversation needs to start now. Get in touch with Neuland's team today to talk through your capacity timeline.
FAQs
1.What methods are used in peptide manufacturing?
Peptide manufacturing relies on a few core synthesis methods:
- Solid-phase synthesis (SPPS): Builds the chain on a resin support, step by step
- Solution-phase synthesis (LPPS): Assembles the peptide in solution, often for shorter sequences
- Hybrid synthesis: Joins fragments built separately, used for longer or more complex peptides
Manufacturers combine these based on the molecule's length and scale.
2.Is peptide manufacturing usually outsourced or built in-house?
Most pharmaceutical companies outsource peptide manufacturing to a specialized CDMO rather than building their own facility. A dedicated plant costs tens of millions of dollars and takes years to validate. A CDMO partner offers established reactors and chemistry expertise without that upfront investment.
3.What does GMP mean in the context of peptide manufacturing?
GMP, or current Good Manufacturing Practice, sets the quality standards facilities must follow. It covers raw material sourcing, equipment qualification, and batch documentation. Regulators, including the FDA, EMA, and PMDA, inspect facilities against these standards before allowing commercial supply.
4.What safety measures apply during peptide manufacturing?
Facilities follow strict protocols given the chemistry involved:
- Careful handling of flammable solvents used in synthesis and purification
- Temperature control for exothermic reactions that can run away if unmanaged
- Containment systems for high-potency compounds, protecting workers on the line
These measures keep facilities safe and inspection-ready.
This article is paid content. It has been reviewed and edited by the Pharmacy Biz editorial team to meet our content standards.